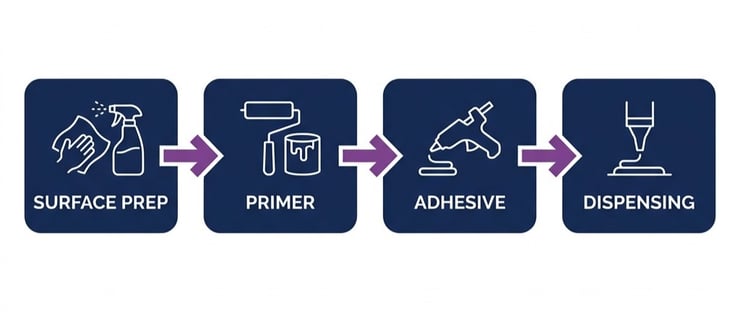
In aerospace assembly, a structural bond is rarely the result of a single product. Depending on the application and qualified process, successful bonding may involve four closely connected considerations: surface preparation, primer, adhesive, and dispensing.
This guide explains why bonding should be approached as a system rather than a shopping list, walks through each of the four steps and how they depend on one another, and sets out the practical decisions that keep a bond strong, durable, and repeatable.
Why Bonding Is a System, Not a Product
The instinct is to focus on the adhesive, because that is the product doing the visible job of holding two parts together. But adhesion is an interface phenomenon. The strength you actually get depends on what is happening at the surface, how that surface is protected and activated, and how cleanly the adhesive is mixed and applied.
Each step sets up the next. Surface prep creates a receptive surface; the primer protects and stabilizes it while improving adhesion; the adhesive forms the structural bond; and dispensing governs whether the adhesive cures and performs as designed. Change one and you often have to revisit the others. That interdependence is the whole reason bonding is qualified as a process, not a part.
Step 1: Surface Preparation
Surface preparation creates the clean, active, and receptive surface a bond depends on. Because adhesion happens at the surface, contamination, oxide layers, or improper surface energy can prevent a strong adhesive from bonding effectively. Preparation typically combines cleaning, abrasion, and chemical treatment matched to the substrate.
Surface preparation can be a major contributor to bond failures. Contaminants such as grease, release agents, and loose oxide can interfere with adhesion and compromise bond performance.
The right method depends on the substrate. Common approaches include:
- Solvent or aqueous cleaning to remove oils, fingerprints, and processing residues. Surfaces are verified using tests like a water-break-free test before proceeding.
- Mechanical abrasion to remove weak surface layers and increase bonding area.
- Chemical treatment such as conversion coatings or etch processes to create a durable, active surface, particularly on aluminum and titanium.
Whatever the method, the prepared surface has a limited active life and must move to priming or bonding before it degrades or re-contaminates. Surface prep and the steps that follow are time-linked, which is exactly why they are validated together.
Step 2: Primer
A bonding or corrosion-inhibiting primer bridges the prepared surface and the adhesive. It protects the freshly treated surface, improves and stabilizes adhesion, and on metals often inhibits corrosion at the bondline. Primers such as BR-127 are matched to specific adhesives and qualified as part of the bonding process.
Once a surface is prepared, it is vulnerable. When a primer is part of the specified bonding process, it helps protect the prepared surface and provides a consistent interface for the adhesive. On metals, a corrosion-inhibiting primer also defends the bondline against the corrosion that would otherwise creep in and undermine the joint over its service life.
Primers are not interchangeable. They are developed and qualified to work with particular adhesives and surface treatments, with defined application and cure requirements. A widely used example in aerospace structural bonding is Solvay BR-127 corrosion-inhibiting primer, which is paired with epoxy film and paste adhesives in qualified processes. The primer you choose has to match both the surface beneath it and the adhesive above it.
Step 3: Adhesive
The adhesive forms the structural bond, but it is qualified as part of a process with a specific surface preparation and primer. Aerospace adhesives include epoxy paste, epoxy film, and urethane chemistries, each suited to different joints, loads, and cure conditions. Substitutions must be validated, not assumed.
With the surface prepared and primed, the adhesive does its job. Aerospace bonding draws on several chemistries, each with a place:
- Epoxy paste adhesives – versatile, high-strength, two-part adhesives for general structural bonding and repair.
- Epoxy film adhesives – supported films that cure under heat and pressure for large-area, high-consistency bonds such as honeycomb and laminate structures.
- Urethane and specialty adhesives – chosen for flexibility, specific environmental resistance, or substrate compatibility.
The critical point is that the adhesive is selected as part of the system. An adhesive such as Loctite EA 9394 epoxy paste adhesive or a film adhesive such as Solvay FM 73 epoxy film adhesive have specific surface preparation, cure, and, where applicable, primer requirements. Swap the adhesive and you may change every other step, which is why substitution has to be validated against the process specification rather than treated as a like-for-like swap.
Step 4: Dispensing
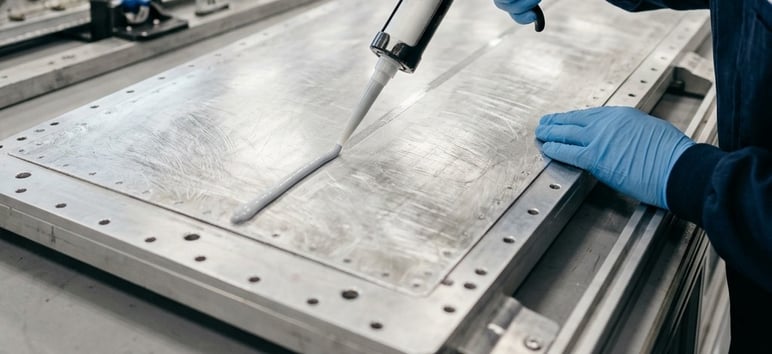
Dispensing controls mix ratio, mix quality, and application of the adhesive. Incorrect ratio or poor mixing of a two-part adhesive prevents full cure, and inconsistent application causes voids and weak spots. The dispensing method must match the adhesive, the joint geometry, and the production volume to deliver a repeatable bond.
Dispensing can be an overlooked part of the bonding process, yet it plays an important role in whether a correctly selected two-part adhesive performs as intended. A two-part adhesive that is mixed off-ratio or incompletely will not reach full cure, regardless of how good the chemistry is. Apply it unevenly and you introduce voids, starved areas, and stress concentrations.
Getting dispensing right means matching the method to the job:
- Mix ratio and mix quality – static mixers, meter-mix equipment, or pre-measured packaging help achieve the specified mix ratio and mix quality. .
- Application control – consistent bead size, coverage, and placement for a uniform bondline.
- Working time and volume – the method should suit the adhesive's pot life and the production rate, from low-volume repair to series assembly.
The right dispensing approach turns a good adhesive into a consistent, repeatable bond, which is the entire objective of treating bonding as a system.
How the Four Steps Depend on One Another
The clearest way to see the system is to follow a change through it. Switch the adhesive, and the qualified surface prep and primer may no longer apply, and the dispensing method may need to change to suit a different mix ratio or pot life. Skip a cleaning step, and even the best primer and adhesive bond to a weak surface layer. Mis-dispense a two-part adhesive, and a perfect surface and primer still yield an under-cured joint.
|
Step |
What it controls |
Depends on |
|---|---|---|
|
Surface prep |
Cleanliness, surface activity |
Substrate and timing |
|
Primer |
Surface protection, adhesion, corrosion |
Surface prep and adhesive |
|
Adhesive |
Structural strength |
Surface prep, primer, cure |
|
Dispensing |
Mix ratio, mix quality, application |
Adhesive and joint |
None of these steps stands alone. The reliability of the finished bond is set by the weakest link in the chain, which is why the steps are qualified, documented, and controlled together.
Common Bonding Mistakes We See
Across aerospace assembly and repair, the same avoidable errors recur, and almost all of them come from treating the four steps as separate decisions:
- Under-investing in surface prep. Rushing or skipping required surface preparation can significantly compromise bond performance.
- Exceeding the surface's active life. Letting a prepared surface sit too long before priming or bonding.
- Mismatching primer and adhesive. Using a primer that was not qualified with the chosen adhesive.
- Substituting adhesives without revalidating. Assuming a like-for-like swap when the prep, primer, and cure may all change.
- Neglecting dispensing. Off-ratio mixing, poor mix quality, or inconsistent application undoing a correct material choice.
A Practical Bonding-System Checklist
Before committing to a structural bond, confirm:
- Substrate and process specification identified, including any engineering or OEM requirement.
- Surface preparation method matched to the substrate, with its active-life window understood.
- Primer qualified with both the surface treatment and the chosen adhesive.
- Adhesive selected for the joint, loads, and cure conditions, as part of the validated process.
- Dispensing method matched to the adhesive's mix ratio, pot life, and production volume.
- Documentation covering materials, batches, shelf life, and process steps for traceability.
How Graco Roberts Supports the Whole Bonding System
Graco Roberts supplies materials across every step of the bonding system, from surface treatments and primers to structural adhesives, sealants, and the dispensing support that ties them together. That single-source breadth makes it easier to keep a process consistent and controlled rather than assembling it from disconnected suppliers.
- Structural and specialty adhesives across epoxy, film, and urethane chemistries in the adhesives range.
- Primers and surface treatments within the coatings range, including corrosion-inhibiting bonding primers.
- Sealants for sealing, environmental protection, and combined seal-and-bond applications in the sealants range.
Pairing the right materials with the right process, and keeping them matched, is what turns four separate products into one dependable bond.
Getting the Whole System Right
A structural bond is built from four interdependent steps: surface preparation, primer, adhesive, and dispensing. Surface prep creates a receptive surface, the primer protects and stabilizes it, the adhesive carries the load, and dispensing ensures the adhesive cures and applies as designed. The bond is only as good as the weakest of those steps.
Approach bonding as a validated system, match each step to the others, and document the process, and you get a bond that is strong, durable, and repeatable. Treating the elements as separate decisions can increase the risk of bond inconsistencies, rework, and other process issues.
For help specifying a complete bonding process or matching materials across the system, contact the Graco Roberts technical team.
Frequently Asked Questions
Why is aerospace bonding treated as a system?
A structural bond is only as reliable as its weakest element. Surface preparation, primer, adhesive, and dispensing are interdependent: a strong adhesive cannot compensate for poor surface prep, and the right primer cannot save a contaminated surface. Treating them as one validated system is what makes a bond repeatable.
Why is surface preparation so important for adhesive bonding?
Adhesion happens at the surface, so the condition of that surface controls bond strength and durability. Contamination, oxide layers, or the wrong surface energy can cause adhesive failure even with a high-performance adhesive. Cleaning, abrasion, and chemical treatment create the active, receptive surface a bond needs.
What does a bonding primer actually do?
A bonding or corrosion-inhibiting primer bridges the prepared surface and the adhesive. It protects the freshly treated surface, improves and stabilizes adhesion, and on metals often inhibits corrosion at the bondline. Primers such as BR-127 are matched to specific adhesives and processes.
Can you substitute one structural adhesive for another?
Not freely. Adhesives are qualified as part of a process with a specific surface preparation and primer. Changing the adhesive can change the required prep, primer, cure schedule, and dispensing method, so substitutions must be validated against the engineering or process specification.
Why does the dispensing method affect bond quality?
Dispensing controls mix ratio, mix quality, and how the adhesive is applied. Incorrect ratio or poor mixing of a two-part adhesive prevents full cure, and inconsistent application causes voids and weak spots. The dispensing method must match the adhesive, the joint, and the production volume.